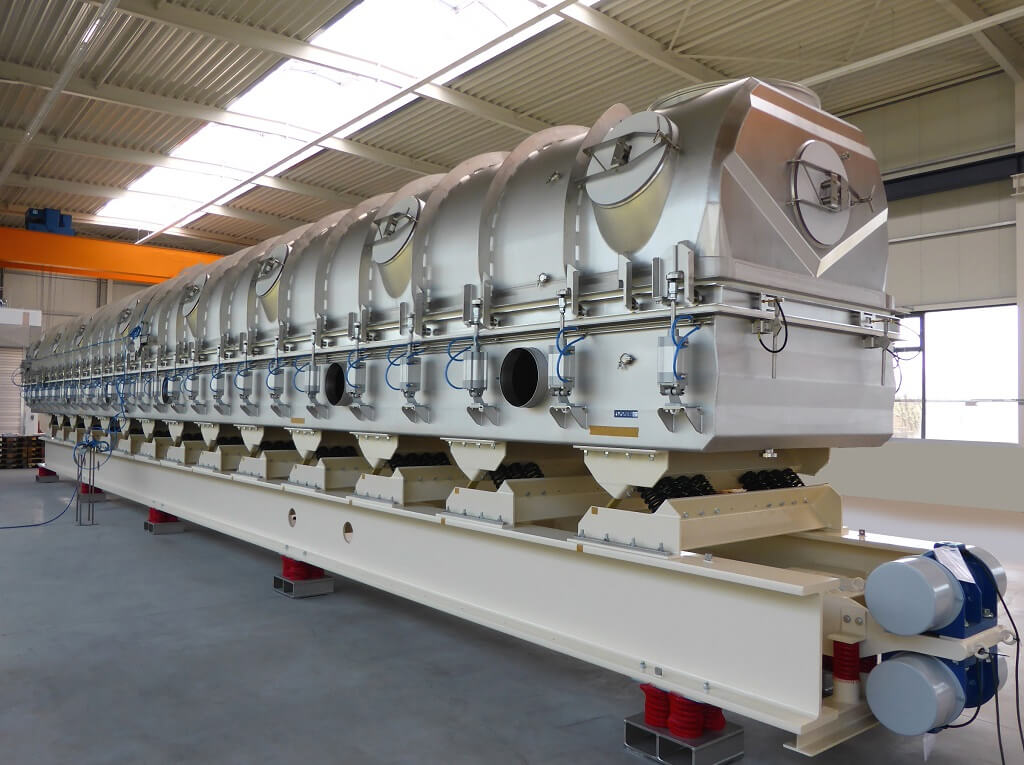
Fluid bed drying is widely used across industries such as pharmaceuticals, chemicals, food processing, and advanced materials due to its efficient heat and mass transfer.
However, despite its advantages, fluid bed dryers can encounter several operational challenges that affect product quality, energy efficiency, and process stability.
This article focuses on the 10 most common problems in fluid bed drying and provides practical, actionable solutions.
1. Uneven Drying
One of the most frequent issues in fluid bed drying is uneven drying, where some particles are overdried while others remain moist. This leads to inconsistent product quality and potential rejection of batches.
Causes
- Poor airflow distribution across the bed
- Channeling or dead zones in the drying chamber
- Wide particle size distribution
- Improper bed loading height
Solutions
- Optimize air distribution design: Use perforated plates or air distributors that ensure uniform airflow across the bed.
- Control particle size distribution: Pre-screen materials to maintain uniformity and avoid segregation.
- Adjust bed height: Maintain an optimal bed depth to allow proper fluidization without restricting airflow.
- Use internal baffles: Improve mixing and eliminate dead zones.
2. Agglomeration and Particle Clumping
Particles stick together during drying, forming lumps or agglomerates. This affects flowability, downstream processing, and product consistency.
Causes
- High moisture content at the initial stage
- Excessive temperature causing surface melting or stickiness
- Inadequate fluidization velocity
- Presence of sticky or hygroscopic materials
Solutions
- Control inlet air temperature: Avoid overheating that can soften or melt particle surfaces.
- Optimize airflow velocity: Ensure sufficient fluidization to keep particles separated.
- Use anti-caking agents: Especially for hygroscopic powders.
- Stage drying process: Start with lower temperatures to remove surface moisture gradually.
3. Channeling and Poor Fluidization
Instead of uniform fluidization, air passes through specific paths (channels), leaving parts of the bed poorly fluidized.
Causes
- Improper air velocity (too low or too high)
- Blocked or damaged air distributor plate
- Uneven particle size or density
- Incorrect equipment design
Solutions
- Maintain proper air velocity: Ensure it is above the minimum fluidization velocity but below the entrainment limit.
- Regular maintenance of distributor plates: Clean and inspect for blockages.
- Improve material consistency: Avoid mixing particles with significantly different sizes or densities.
- Upgrade distributor design: Use multi-hole or bubble-cap distributors for better airflow uniformity.
4. Excessive Dust Generation and Product Loss
Fine particles may be carried away by the airflow, leading to material loss, contamination, and environmental concerns.
Causes
- High air velocity
- Large proportion of fine particles
- Inadequate dust collection system
- Poor cyclone or filter performance
Solutions
- Optimize airflow rate: Avoid excessive velocities that entrain particles.
- Install efficient dust collection systems: Use cyclones, bag filters, or HEPA filters.
- Pre-classify particles: Remove excessive fines before drying.
- Implement product recovery systems: Reintroduce collected fines into the process if applicable.
5. Overheating or Thermal Degradation
Heat-sensitive materials may degrade, discolor, or lose functionality due to excessive temperatures.
Causes
- High inlet air temperature
- Poor temperature control systems
- Long residence time
- Uneven heat distribution
Solutions
- Use precise temperature control systems: Implement automated feedback loops.
- Lower drying temperature: Especially for sensitive materials such as pharmaceuticals or polymers.
- Reduce residence time: Increase airflow efficiency to shorten drying duration.
- Consider multi-stage drying: Combine low-temperature pre-drying with final drying stages.
6. High Energy Consumption
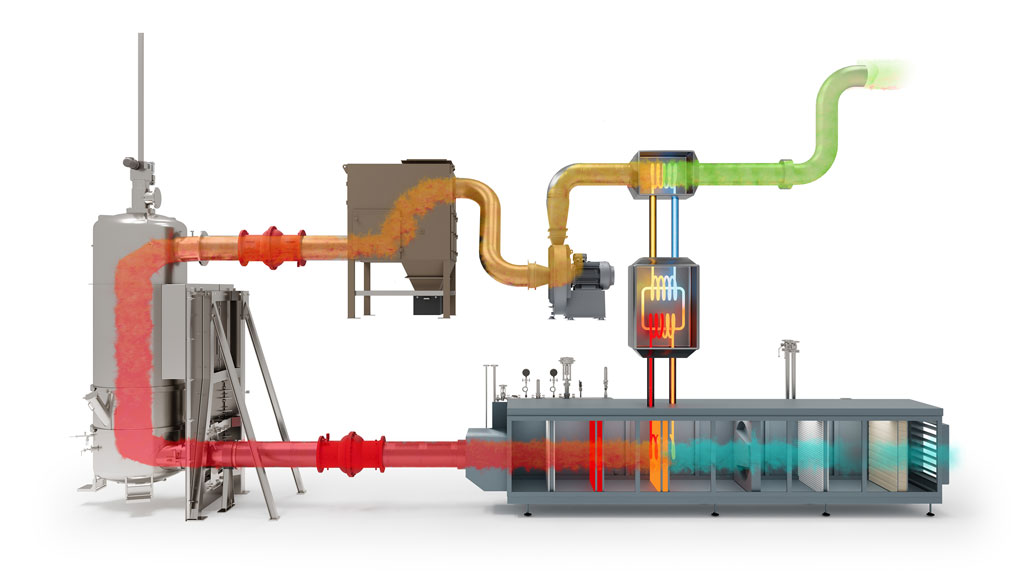
Fluid bed dryers can consume significant energy, especially when not optimized, leading to higher operational costs.
Causes
- Inefficient heat utilization
- Heat loss through exhaust air
- Overdrying of materials
- Poor insulation
Solutions
- Recover exhaust heat: Use heat exchangers to recycle energy.
- Improve insulation: Minimize heat loss from the system.
- Optimize drying endpoint: Use moisture sensors to prevent overdrying.
- Adopt variable frequency drives (VFDs): Adjust fan speed based on process needs.
7. Defluidization (Bed Collapse)
The fluidized bed suddenly collapses, stopping proper drying and causing process interruption.
Causes
- Sticky or wet materials forming bridges
- Insufficient airflow
- Equipment malfunction
- Excessive bed load
Solutions
- Maintain proper airflow: Ensure consistent air supply above minimum fluidization velocity.
- Control feed rate: Avoid overloading the bed.
- Pre-condition materials: Reduce initial moisture if necessary.
- Use mechanical agitation: Prevent bridging and improve flow.
8. Electrostatic Charging
Static electricity builds up during drying, causing particles to stick to equipment walls or creating safety hazards.
Causes
- Dry air conditions
- Fine powders
- Non-conductive materials
- High airflow velocities
Solutions
- Install grounding systems: Ensure all equipment is properly grounded.
- Control humidity levels: Slightly increase humidity to reduce static buildup.
- Use antistatic materials or coatings: In equipment design.
- Reduce excessive airflow velocity: Minimize friction-induced charges.
9. Equipment Fouling and Cleaning Challenges
Material buildup inside the dryer reduces efficiency and increases downtime due to frequent cleaning requirements.
Causes
- Sticky or resinous materials
- Incomplete drying
- Poor airflow distribution
- Inadequate cleaning systems
Solutions
- Use non-stick coatings: Reduce adhesion of materials to surfaces.
- Optimize drying parameters: Prevent partially dried sticky states.
- Install Clean-in-Place (CIP) systems: Enable efficient and automated cleaning.
- Improve airflow design: Reduce areas where material can accumulate.
10. Inconsistent Product Quality
Variations in moisture content, particle size, or temperature lead to inconsistent final product quality.
Causes
- Fluctuations in feed rate or material properties
- Poor process control
- Inadequate monitoring systems
- Environmental variations
Solutions
- Implement real-time monitoring: Use sensors for moisture, temperature, and airflow.
- Automate process control: Maintain stable operating conditions.
- Standardize raw materials: Ensure consistent input quality.
- Use data analytics: Continuously optimize process parameters.
TROUBLESHOOTING REVIEW
Use Process Data Before Changing a Fluid Bed Dryer
Many fluid-bed symptoms have more than one possible cause. Before changing airflow, temperature, feed rate or equipment settings, record the material behavior and operating data so the problem can be separated from the proposed remedy.
Record the operating condition
- Feed rate, initial and target moisture, particle-size distribution and bulk density
- Inlet and outlet air temperature, airflow and pressure observations
- Bed behavior, residence time, product temperature and discharge consistency
- Dust collection, filter condition, deposits and any visible carryover
Check material changes first
Changes in particle size, moisture, formulation, feed consistency or fines can affect fluidization and drying response. Compare the current material with the conditions under which the dryer previously operated acceptably.
Escalate safety-relevant symptoms
Unexpected temperature rise, combustible-dust concerns, solvent changes, abnormal pressure behavior or equipment damage should be assessed under the site safety procedure before process adjustments are made. The correct response depends on the actual material, equipment and applicable requirements.
Troubleshooting boundary: These checks are general engineering guidance, not remote operating instructions or a guarantee of correction. Any change to operating conditions, safety measures or equipment should be evaluated by qualified personnel using the actual process data.
Related Fluid Bed Drying Equipment
Discuss a Fluid Bed Drying Problem
Send the material description, current operating data, observed symptom, production target and available layout or equipment details for a focused engineering review.
Fluid Bed Troubleshooting FAQs
What data is most useful when drying becomes uneven?
Record feed moisture and rate, particle information, inlet and outlet conditions, airflow, bed behavior, residence time, product temperature and collection observations.
Can higher air temperature solve every drying problem?
No. Higher temperature can change product behavior and may not address airflow distribution, feed condition, bed fluidization or collection issues. The cause should be identified first.
Why can the same dryer behave differently with a new material batch?
Changes in moisture, particle distribution, fines, bulk density, formulation or flow behavior can alter fluidization and heat-transfer response.
When should an engineering review be requested?
Request review when a symptom persists after normal checks, production conditions change materially, or the issue may involve product quality, safety, dust collection, deposits or equipment damage.
Fluid Bed Dryer Troubleshooting: Start with Evidence
Fluidization problems should be diagnosed from process data rather than a single symptom. Record feed condition, airflow, pressure drop, temperature, moisture, product movement, fines, alarms and recent operating changes before adjusting the equipment.
Separate material, air and equipment causes
Check particle-size distribution, density, cohesion, moisture and feed rate alongside distributor condition, fan performance, filters, heaters, dampers, sensors and controls. Channeling, defluidization, agglomeration or dust may have more than one cause.
Use safe, controlled adjustments
Define allowable temperature, pressure, airflow and feed-rate limits. Change one variable at a time, document the result, inspect for buildup or wear and follow the approved operating and lockout procedures. Do not bypass alarms, guards or interlocks.
Escalate recurring issues to engineering review
Persistent uneven drying, high dust, overheating, abnormal pressure drop, product damage or unstable discharge may require sampling, airflow testing, distributor inspection, control review or a project-specific redesign.
Safety boundary: this guide is not a substitute for the equipment manual, site risk assessment, applicable regulations or qualified maintenance personnel. No troubleshooting step guarantees a result; isolate energy sources and obtain responsible approval before intrusive work.
Prepare a Fluid Bed Dryer Troubleshooting Inquiry
Send equipment model, material data, feed and discharge rates, trend records, pressure and temperature readings, alarms, photos, filter condition, recent changes and the desired outcome. Review the fluid bed systems, working principle, equipment diagram and contact requirements.
Request Fluid Bed Troubleshooting Support
Fluid Bed Dryer Troubleshooting FAQs
What data should be collected first?
Record material condition, feed rate, airflow, pressure drop, temperatures, moisture, alarms, product movement and recent changes.
Can airflow alone solve uneven drying?
Not necessarily. Distributor condition, feed behavior, loading, temperature, residence time and controls may all contribute.
When should operation be stopped?
Follow the site risk assessment and manual; stop and escalate for unsafe temperature, pressure, dust, guarding, electrical or abnormal mechanical conditions.
What helps diagnose a recurring problem?
Trend data, representative samples, inspection records, maintenance history, photos and a documented sequence of operating changes.